 Back to news
5 MES solutions to address industry challenges
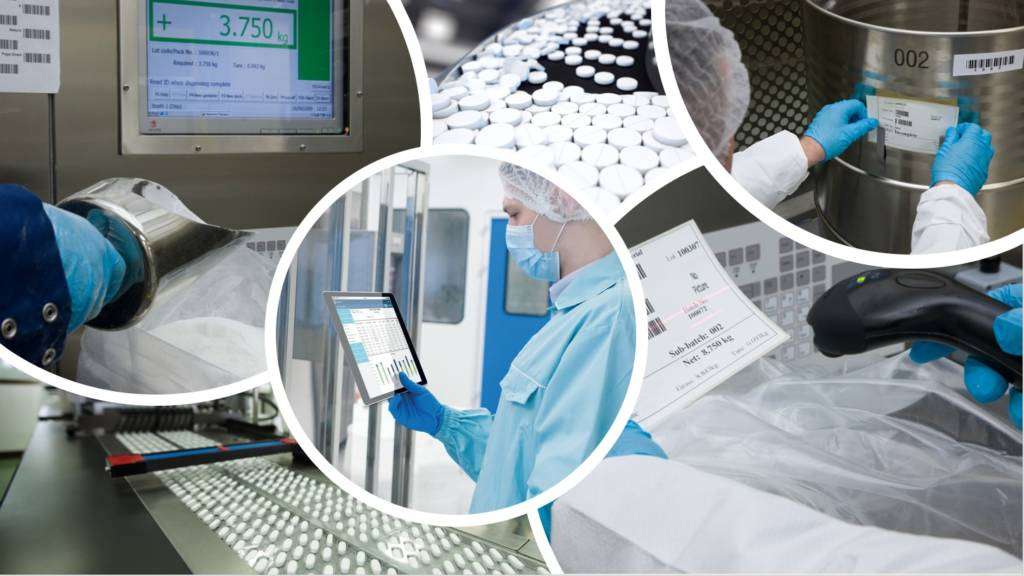
Pharmaceutical manufacturers operate in an increasingly competitive, fast-moving environment. Integrated continuous manufacturing, individualised medicine, counterfeiting protection, and a focus on product quality are just some of the trends creating new pressures. The right MES solutions can address many of these complex challenges by providing real-time visibility, enabling better process understanding, faster issue resolution, and improved decision-making.
1. Quality Challenges
With paper-based systems, companies can maintain high quality; however, this level of quality comes at a high cost. An MES reduces the cost of quality while ensuring no drop in quality. MES enforces compliance across many aspects of manufacturing, including Standard Operating Procedures.
Automating manual operations and validating all data entry minimises the risk of errors. If discrepancies occur, the system flags them immediately and halts the process, preventing production delays and batch failures.
2. Production Challenges
The more products handled in production or packaging, the less effective paper-based systems become. Not all batch records are completed “Right First Time”, which, alongside batch failures and errors being identified too late, are all disadvantages of the paper-based production process. These issues can be eliminated with the right MES solutions.
Reviews of paper-based batch records can also be frustratingly slow. An Electronic Batch Record dramatically shortens the production release process — every step is automatically verified, saving time by working by exception, as operators are alerted to omissions and exceptions.
3. Cost Challenges
From low-cost generics to high-margin, specialised drugs, everyone is working to make manufacturing more efficient, less costly, and more consistently reliable.
With the introduction of an MES, the largest cost savings come from streamlining manual processes, reducing staff costs, minimising the risk of scrapped production and disposal costs, and significantly reducing inventory levels through real-time stock movements and updates.
4. Compliance Challenges
Inspectors policing large pharma markets closely examine underlying recordings, systems, and data handling. Data integrity is receiving the highest attention in the industry because of the risks of failing to meet the latest regulatory expectations for counterfeiting, tampering, and traceability. MES directly reduces the risk of data integrity issues and audit failures and therefore has a major impact on compliance records.
5. Data Analysis Challenges
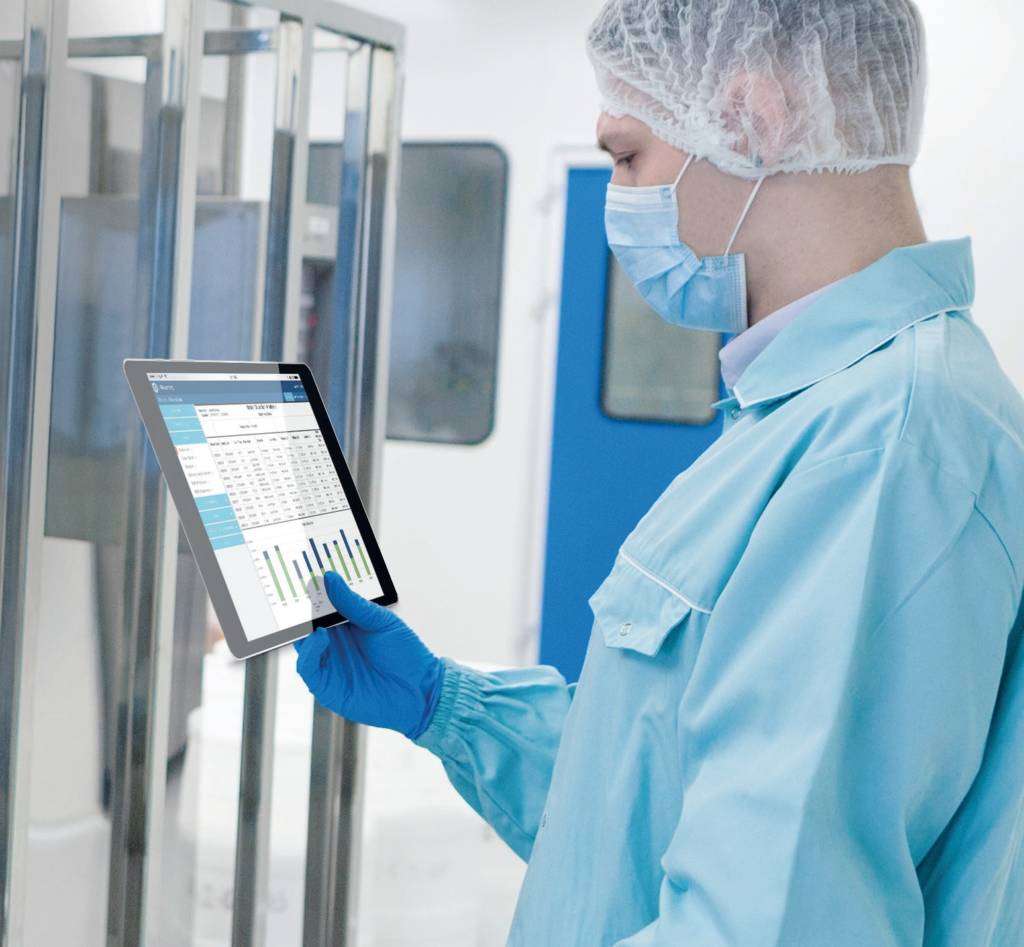
The volume of paper-based data collected in a pharmaceutical manufacturing operation is staggering, yet research shows that much of this information is rarely used beyond compliance. Data access with paper systems is at best problematic for assessing current product status or analysing historic batch results. Manufacturers can use MES technologies and the information they provide to understand and improve their processes.
With MES solutions, you gain real-time visibility on operations and processes. Real-time information from the manufacturing process is needed to prevent problems, drive quality, and enable the flexibility your customers require. MES enables this reach into the manufacturing process and is seen as a key requirement for successful Business Process Management.
MES Solutions can Help Address Your Industry Challenges
MES solutions don’t just help you implement manufacturing operations — a superior solution can even help you tackle industry challenges and lead you to outperform competitors. In this article, we summarised some of the key industrial challenges that an MES can help address:
- Quality Challenges – minimise the cost of quality
- Production Challenges – ensure it is “Right First Time”
- Cost Challenges – make better use of your resources
- Compliance Challenges – lower the risk of data integrity issues
- Data Analysis Challenges – gain real-time visibility on operations
We hope our article was helpful in highlighting how choosing the right MES technology can help manage these industry pressures. If you would like to learn more about our MES solution or discuss an MES implementation project, please contact our specialist team here.